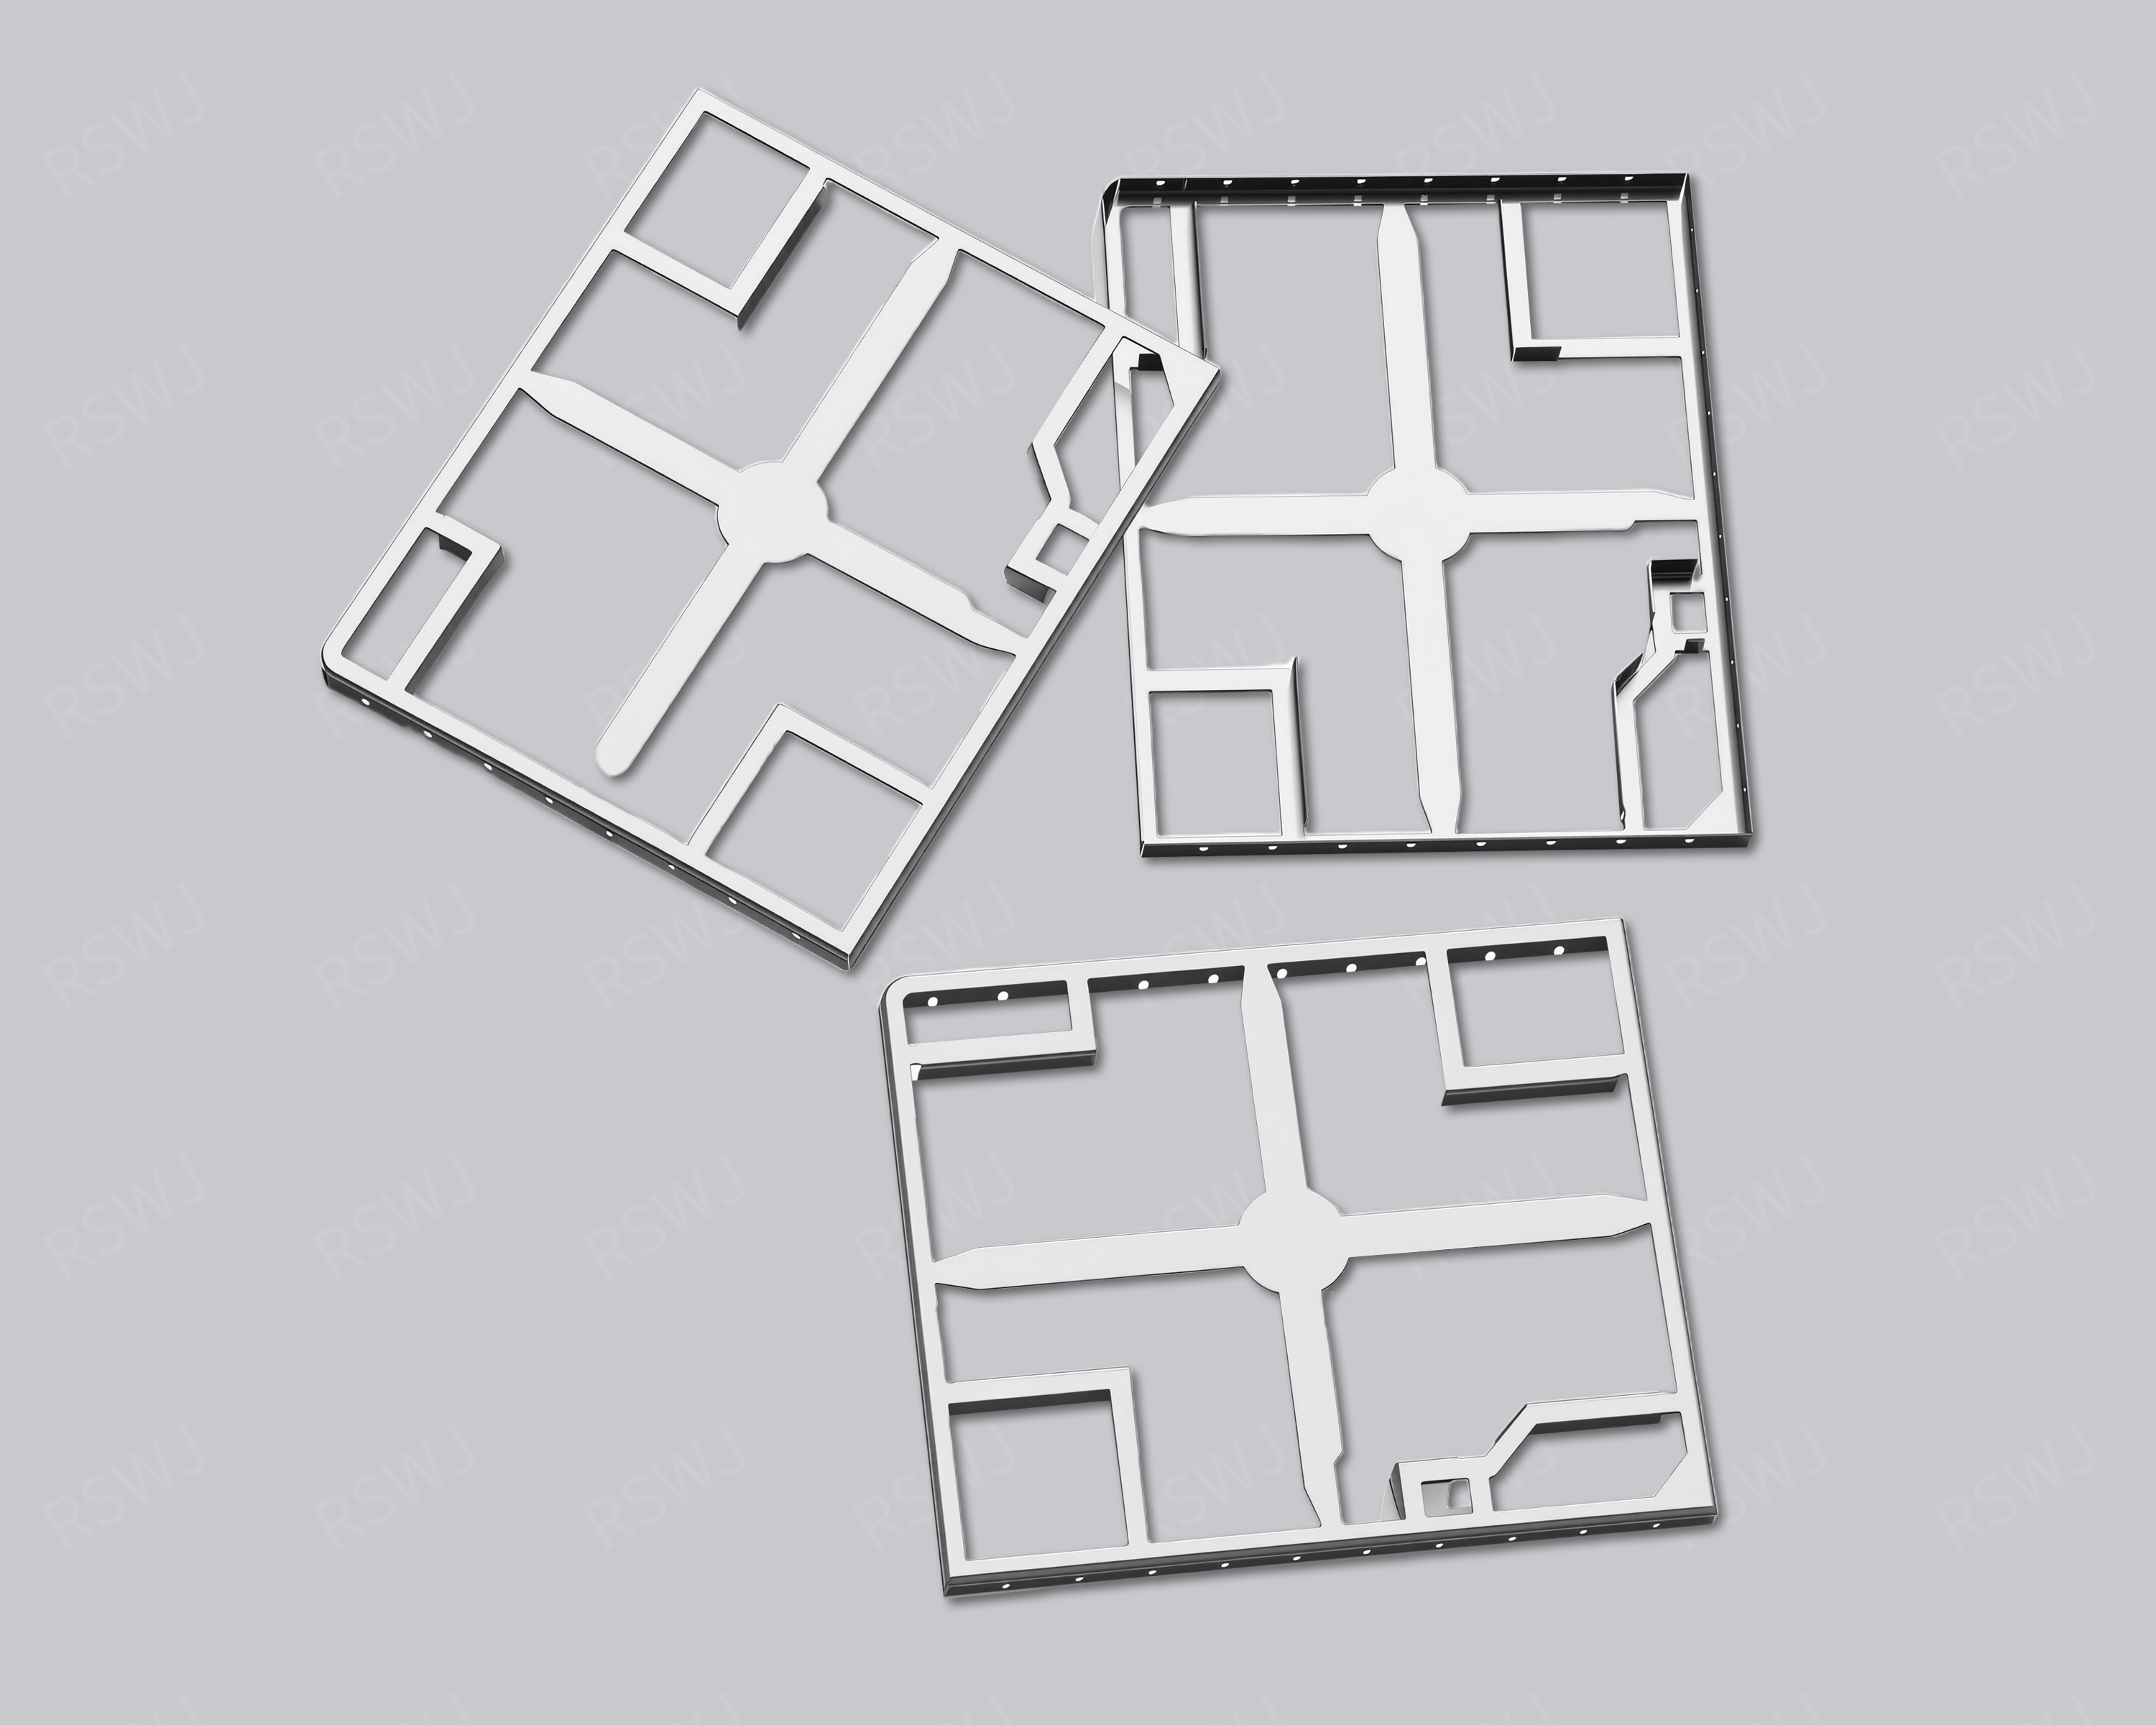
Reference photograph. Material, dimensions and mating requirements are defined in the agreed project drawings.
Steel and tin surface after forming
A tinplate shield combines a steel substrate with a tin-coated surface in a formed component.
| Design focus | Steel substrate, tin surface, cut edges and board attachment region |
|---|---|
| Project task | Steel and tin surface after forming |
| Custom inputs | Current drawings, mating parts, material and final surface, quantity and acceptance requirements. |
Steel and tin surface after forming
Steel and coating have different roles in the part definition. The material name does not specify thickness, condition or the final attachment-edge requirement.
Specify the tinplate substrate and coated surface as linked but separate material inputs. Review cut edges, bends and attachment areas in the formed condition. Packaging and handling should preserve the edges and surfaces used during installation. If later processing is introduced, keep its relationship with the original coating clear. Inspect the sample in the final treatment state and use the customer assembly conditions for any joining evaluation, rather than accepting the material name as a complete specification.
Engineering considerations for this project
Specify the steel substrate and tin surface together
A tinplate shielding component combines a specified steel substrate with a tin-coated surface, so both inputs should remain identifiable in the material requirement. State the customer’s designation and supplied condition rather than using the general tinplate name as the complete procurement specification. Clarify the required finished geometry and whether any later process changes the surface state. This distinguishes a part made from the selected material from a separate proposal to apply tin treatment to another substrate. The manufacturer can then review the forming and interface requirements against a known material input instead of substituting a similar-looking metal without a defined approval basis.
Locate the attachment and mating regions that make the surface important to the assembly. State the customer’s joining or contact requirements where they apply and distinguish them from appearance requirements elsewhere on the component. The substrate and coated surface have linked roles, but neither the label nor the sample’s color establishes a universal joining condition or coating value. Providing the actual interface purpose allows engineering to review the material and forming route together. It also gives manufacturing a clear reason to preserve a particular edge or surface boundary when a local process or geometry proposal is considered.
Review cut and formed regions in their final state
The finished tinplate part should be reviewed after the operations that establish its working edges, bends and attachment features. Identify where trimming, opening creation or forming changes the geometry involved in assembly. If a cut edge or a formed transition is significant to the customer’s surface requirement, state that requirement explicitly and locate the region against the drawing references. A broad check of the main face can miss the local condition that matters at an attachment edge. The inspection plan should therefore distinguish the general material surface from the specific features that position, close or connect the supplied component.
Compare the sample with the actual partner or board references used by the customer. Examine the final fit and the relevant attachment operation rather than relying only on a loose-part outline. Where joining is part of the project, retain the specified customer conditions and the material version used for the trial. Keep visual, dimensional and joined-interface observations distinguishable in the record. This gives engineering a useful way to identify whether a reported issue concerns the formed contour, a local surface region or the assembly operation, instead of changing the complete material specification to address an unidentified observation.
Preserve the accepted surface through handling and later processes
Discuss how the part is packaged, removed from the supply arrangement and placed into the assembly, focusing on the edges and surfaces used by the project. Identify where loose parts may bear against one another or where the operator grips the component. If those conditions affect a relevant region, include representative received and handled samples in the review. This is a practical supply-and-assembly check tied to the customer’s component, not an assumed durability result. It helps ensure that the part evaluated during manufacturing and the part entering the actual attachment operation are described through comparable conditions.
If a later treatment or material alternative is proposed, identify its relationship with the original tin surface and the finished geometry. Keep the selected substrate, surface version, drawing revision and mating information together in the comparison. A process introduced for one requirement can affect a region used for another, so review the relevant final-state checks before accepting the change. For procurement, state the confirmed tinplate specification, any permitted alternatives and the approval scope explicitly. These inputs support a reproducible shielding-component supply definition without inferring material composition, treatment parameters or validated joining performance from the reference image or the general material name.
Boundary, clearance and mating design
Review cut edges and bends after forming. A joining region may need different checks from a non-contact external surface.
A material comparison is most useful when the geometry and installed interfaces are identified. Mark where the shield lands, where it closes and where signals or connectors cross the boundary. The intended circuit region and operating context remain important even when the search began with an alloy name. A different material is not a substitute for an undefined attachment or opening. Keep those relationships fixed, or explicitly identify them as changes, when evaluating alternatives.
Material and final surface definition
Build the material definition from the applicable grade or standard, supply condition, thickness and final surface. State which requirements are mandatory and which alternatives may be reviewed. If documentation is needed, identify its scope with the project rather than assuming a product photograph supplies it. This separates identity from performance: the material record establishes what was used, while the agreed part and application checks establish the relevant condition of the sample.
Forming and the installation sequence
Clarify whether sheet is supplied with the required coating and whether later treatment is needed. Protect functional edges during handling and packaging.
Review the actual formed features with the material condition. Bends, small corners, cut edges and working retention areas pose different questions from a flat sheet. Specify functional dimensions on the finished component using meaningful datums. If later processing changes a mating surface, inspect the final state. The manufacturing route should be reviewed with the whole drawing package instead of selected from the alloy name without its geometry and installation requirements.
The formed coated sheet is the accepted object
Review the steel substrate and tin surface through the actual forming and attachment route. A cut edge, a formed corner and a joining region may have different observations after manufacturing. Distinguish material supplied with a coating from any later treatment and identify the final delivered surface. If handling affects an important edge, agree a suitable orientation and protection with the assembly and packaging teams before approval.
Part inspection and application evaluation
Inspect material and surface records, formed dimensions and attachment regions. Where soldering is intended, evaluate installation with customer assembly conditions.
A drawing package for this custom part
| Input | What makes it usable |
|---|---|
| Coverage & interfaces | Steel substrate, tin surface, cut edges and board attachment region. Mark their relationship with the actual circuit or mating layout; identify fixed references and permitted changes. |
| Final part & datums | A dimensioned finished-part drawing and available 3D information. Identify functional dimensions, the installed condition and the measurement references used to accept them. |
| Material & surface | The specified grade, condition, thickness and final treatment. Show contact, joining and insulated regions separately; identify any alternative that needs evaluation. |
| Assembly & acceptance | Corresponding mating revisions and the installation or access sequence. Distinguish part inspection, matched fit and customer system checks with their agreed conditions. |
Questions for this design review
What should be checked after bending or trimming?
Inspect the agreed dimensional features and the surface locations relevant to contact or joining. Record the final material and processing condition with the sample. If the customer uses solder attachment, include the actual assembly conditions in the evaluation instead of treating the tinplate name as a complete joining approval. A finish record and an installed check support different acceptance questions and should remain identifiable.
Which drawings support the review of Tinplate EMI Shielding Can?
Use the current layout and mating assembly to identify steel substrate, tin surface, cut edges and board attachment region. Mark the relationship that is already fixed and the specific feature being considered for change. A drawing of the cover alone may omit the condition that gives the reference its engineering purpose. Include the corresponding board or base and the intended operation so the proposed revision can be evaluated against a defined task rather than a similar-looking external shape.
In-House Tooling & Formed-Part Quality
Tooling development and forming quality
The manufacturing review for Tinplate EMI Shielding Can connects how critical features are formed, how they are inspected and how they meet the mating assembly. Ruishuo links in-house die design and CAD/CAM simulation with stamping. Die-making output of more than 100 sets per month is a factory capability; the tool concept is reviewed for the actual project.
Material condition and formed-part behavior
Specify material grade, thickness and supply condition with the tooling inputs. A material change can affect bending, springback and contact features, so matching the old outline is only part of the review. Define the final attachment, opening and engagement requirements.
- Complete material inputs
- Record the specified grade, thickness, condition and finish. For substitutions, agree the acceptable range and affected validation items.
- Checks against the mating assembly
- Keep the material and drawing revision with the sample report. Check the controlled dimensions, then verify the actual attachment and closure.
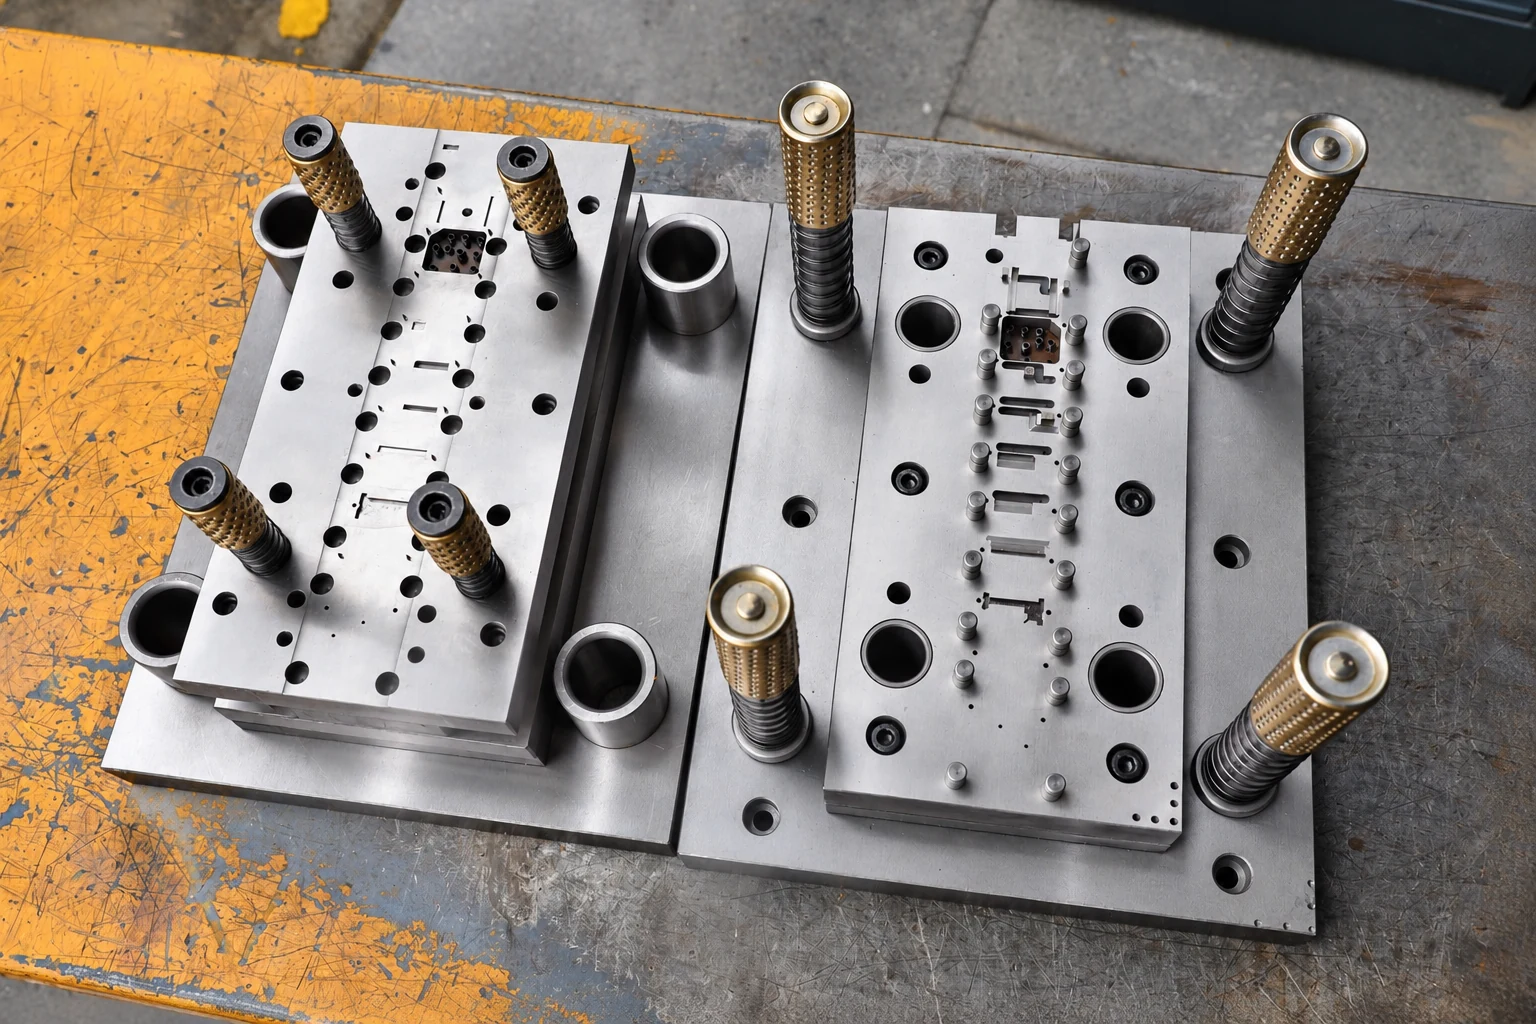
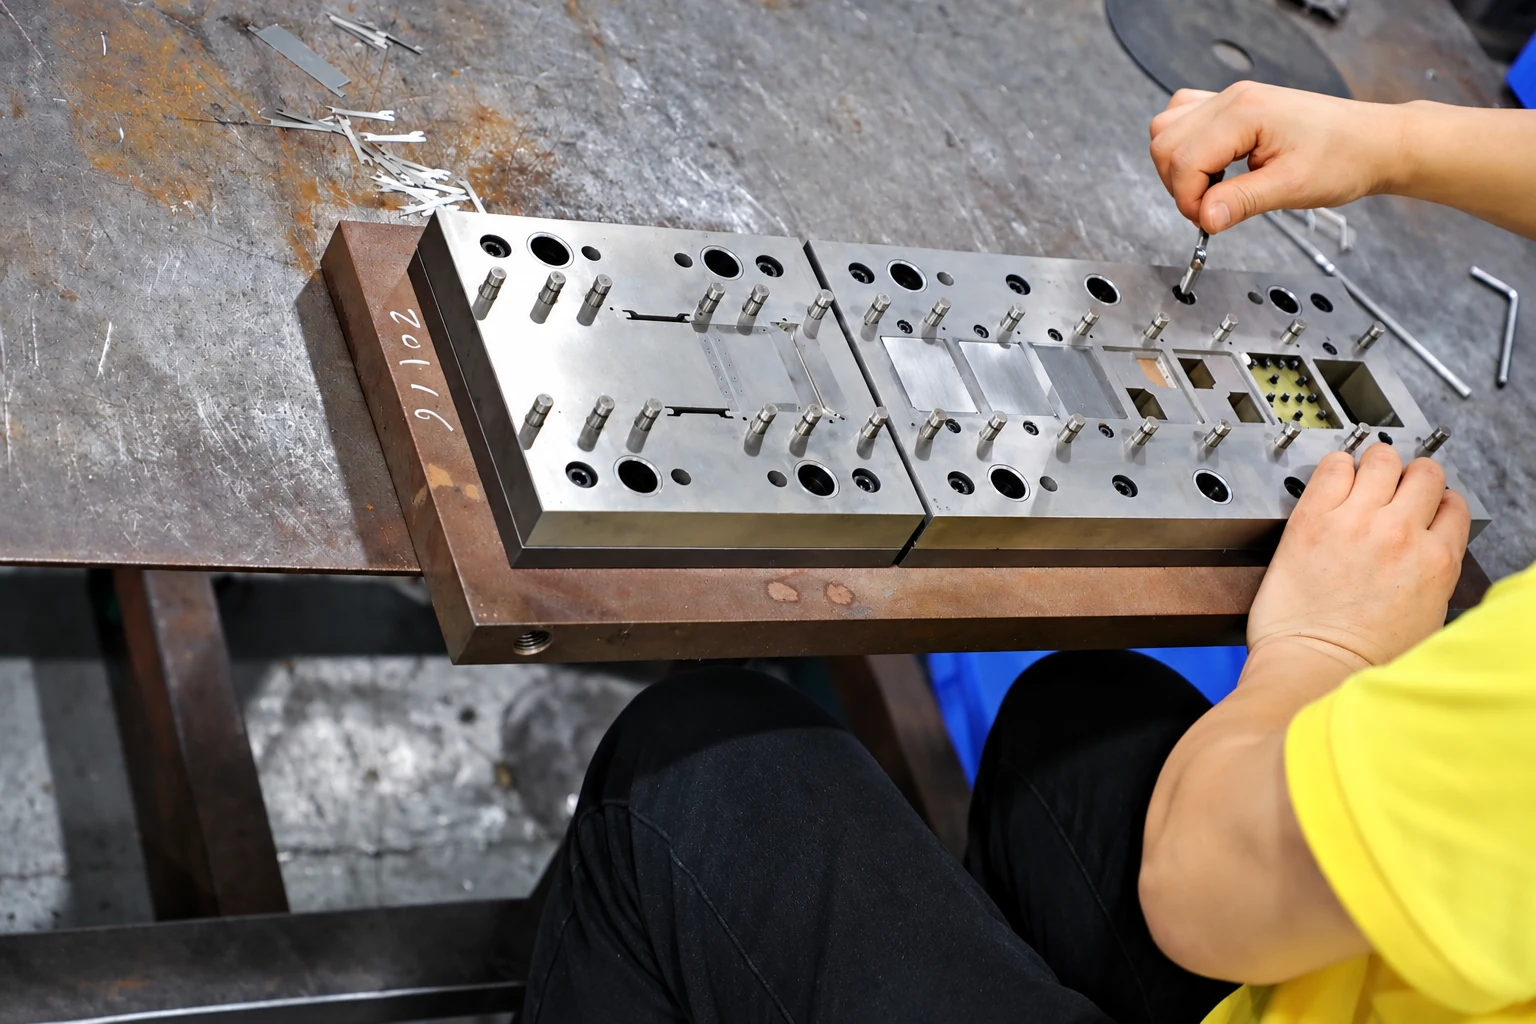
Paid samples include a full dimensional inspection report. Define drawing datums, acceptance criteria and corresponding mating parts so measurement and installed-fit checks can each answer the correct question. Confirm the charges, responsibilities and revision requirements for design changes, tooling work and later production stages within the project scope.
Paid samples and project planning
Samples are chargeable. Reference planning: standard samples 3–5 days; expedited sampling 48 hours; tooling and sample production 7–10 days. These are sample-stage arrangements, excluding mass-production delivery. The project plan is reviewed against the confirmed information, process and sample scope.
Related structures and project directions
Compare references through their coverage, installation and manufacturing tasks.
301 Stainless Steel Shielding Can
A 301 stainless steel shielding can starts with a specified alloy grade and a separately defined material state.
Design & manufacturing details →
Stainless Steel Shielding Can
A stainless steel shielding can requires a specific grade, supply condition and joining arrangement.
Design & manufacturing details →
Permalloy Shielding Cover
A permalloy cover addresses a defined magnetic-field problem with an agreed alloy and treatment condition.
Design & manufacturing details →Discuss your Tinplate EMI Shielding Can project
Send the current drawing and mating conditions so we can review the structure, material, sample scope and required checks.
Send your project requirementsExplore shield materials